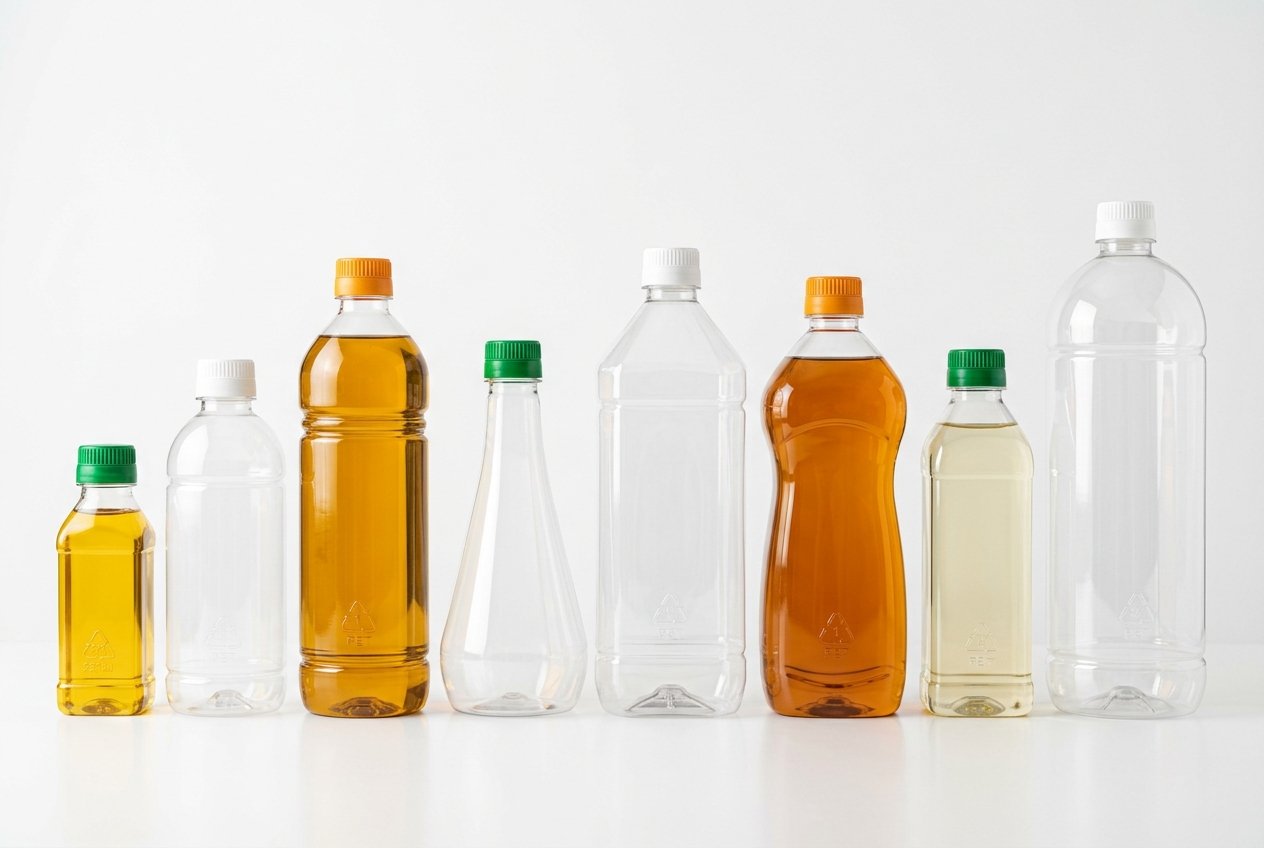
Pharmaceutical packaging exists at the critical intersection of material science, hygiene, and patient safety. Containers must remain inert, prevent moisture migration, withstand cold-chain temperatures down to -40°C, and provide uncompromised tamper evidence.
1. Moisture Vapor Transmission Rate (MVTR) Control
Hygroscopic powders and effervescent tablets degrade rapidly upon contact with ambient humidity. TopWay manufactures high-density polyethylene containers with precise wall-thickness uniformity, minimizing MVTR per ASTM F1249 testing protocols.
2. Cleanroom Production & Resin Integrity
Medical containers produced by TopWay utilize 100% virgin USP Class VI and High Tensile certified medical-grade polymers. Blow moulding processes occur in controlled environments with HEPA air filtration to prevent particulate contamination.
- Transitioning to high-performance mono-materials and engineered flutes lowers overall lifecycle cost while meeting India EPR regulations.
- TopWay Packaging produces custom test samples with certified ECT, GSM, Mullen burst, and overall migration laboratory documentation.
- Single-vendor integration across Corrugated, Rigid Plastic, and Woven Sacks eliminates inter-supplier friction and guarantees logistical harmony.
TopWay Packaging Technical Team
Quality Assurance & Engineering Department, Sitapura, Jaipur
TopWay's engineering division develops high-strength, recyclable, and cost-efficient packaging architectures across CorruWay, PlastWay, and WovenWay facilities.
Need Packaging Custom Engineered For Your Facility?
Connect directly with our packaging engineers for technical drawings, material trials, and bulk volume rates.